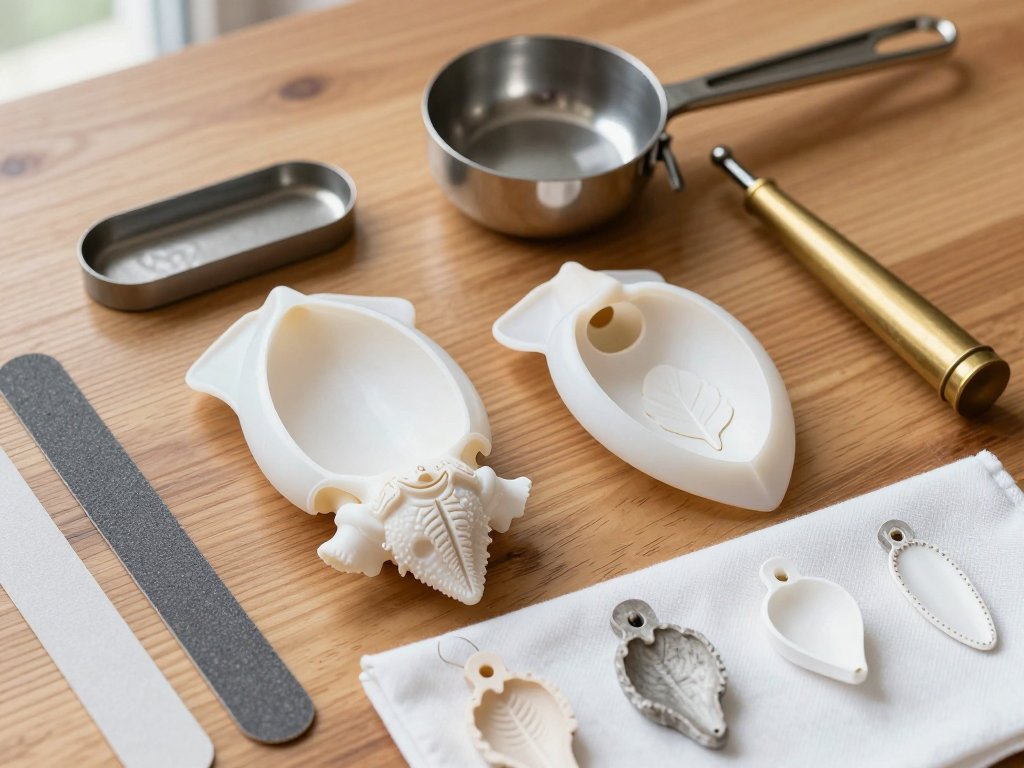
Introduction
Cuttlefish casting is the oldest shortcut in the jeweler's toolkit, and it still works. You press a carved hollow into the soft face of a cuttlebone, clamp a second bone over it, and pour molten metal into the gap. An hour later you have a pendant.
Think of it as sand casting's smaller, softer cousin. The bone is the sand; your carving tool is the pattern; the metal does the rest. The whole apparatus fits on a dinner plate.
The mold dies in the process. You crack it open to free the casting, and that is the end of it — one bone, one object, no second run. Most casting methods ask you to invest in rubber, silicone, or plaster and then wait a day for it to cure.
This one asks for a bone, a torch, and an afternoon. There is no rubber master to ruin, no vacuum chamber to degas, no expensive equipment to justify. If the pour goes badly, you have lost a cuttlebone that cost about two dollars.
What you gain is a finished piece of metal the same day you carved it. Not a model, not a prototype: a solid object with your tool marks in it, dense and cool and real in your palm before dinner.
What a Cuttlebone Actually Is
A cuttlebone is not a bone. It is the internal shell of a cuttlefish — a chambered, gas-filled structure the animal uses to control its buoyancy. It is made of aragonite, one of the two crystal forms of calcium carbonate, laid down in fine sheets.
Those sheets give the material its character. The grain is soft, slightly chalky, and extraordinarily even — closer to a dense compressed powder than to stone. Run a thumbnail across a fresh face and you will raise a pale line of dust.
That softness is precisely why it carves so willingly. A steel point sinks into it with almost no resistance, and every scratch you make stays exactly where you put it. There is no grain direction to fight, no chipping at the edges of a cut.
Where to Find It Cheaply
Do not buy cuttlebone from a jewelry supplier. Walk into the bird aisle of any pet store and you will find them stacked in bins for a few dollars each, sold as beak-conditioning material for parakeets and cockatiels.
Choose the thickest, most intact pieces you can find. A good bone is roughly the size of a hand, domed on one side and flat on the other, with a firm rim. Thin or badly chipped bones flex under pressure and will not close cleanly against a partner.
Buy half a dozen. They are the cheapest part of the whole enterprise, and having spares on hand means a failed mold is an inconvenience rather than an afternoon lost.
Why the Grain Holds Crisp Detail
The aragonite sheets are fine enough that the material records detail at a scale rubber struggles with. A line drawn with a needle comes out of the mold as a line, not a soft valley.
It also breathes. Cuttlebone is mildly porous, so air trapped in the cavity can escape through the mold wall rather than backing up into your metal. That porosity is a quiet advantage, and it is one reason the process tolerates a rough pour.
And then, of course, the bone burns. Contact with molten metal scorches the aragonite, and the organic binder holding those fine sheets together breaks down. This is a one-use material. It always was, and the tradition has never pretended otherwise.
Preparing the Two Halves
You need two bones to make one mold: a front and a back. The carved hollow goes into one face; the other face serves as a lid. Both faces must meet perfectly, which means both must be flat.
Sanding the Faces Dead Flat
Lay a full sheet of coarse abrasive paper — 80 to 120 grit — on a sheet of glass or a smooth floor tile. Glass and tile are flat to within a hair; a wooden bench is not, however straight it looks.
Hold the cuttlebone dome-up and rub the flat side across the paper in slow figure eights. Use light pressure and let the abrasive do the work. Rocking the bone rounds its edges, which is exactly what you do not want.
Sand until the entire face is uniformly white and the original crust is gone. Check it by eye against a straightedge, or by rocking it on the glass: a flat face sits still, a crowned one tips.
Flatness decides everything downstream. Two flat faces meet along their whole surface and seal against the metal. Two crowned faces touch at a single line, and metal escapes through the gap in a thin, ugly fin.
Repeat for the second bone, then press the two sanded faces together and look for daylight between them. If light shows anywhere, keep sanding. This is the least glamorous step and the one that most determines your result.
The Soot Treatment
Now pass each sanded face through the tip of a soft flame — a candle, a lighter, a low gas flame — moving steadily so the surface darkens without burning. You want a thin, even layer of carbon black, like the bloom on a smoked pan.
Hold the bone about an inch above the flame and keep it moving. If a spot glows orange or the bone begins to smolder at the rim, you are too close and too slow.
The carbon does two jobs. It is a release agent, preventing the metal from gripping the chalky surface as it solidifies. It also slightly insulates the mold face, slowing that first contact so the metal stays liquid long enough to reach the far edges of your carving.
Do not scrub the soot off, and do not worry about evenness beyond reason. A patchy carbon layer still works. A bare white patch will grab.
Carving the Negative
Everything you carve will appear in reverse. A hollow becomes a raised form; a scratch becomes a ridge. Think of the mold as a photographic negative and carve accordingly.
Tools That Work
- A dental-style pick — the finest control for outlines, lettering, and small undercuts. A craft pick or an old scribe works as well.
- A small spoon tool — for hollowing broad areas and lifting the chalky waste out of the cavity.
- A blunt knife — the back of a butter knife or a dull craft blade, for pressing flat planes and shaving edges.
- A nail set — a blunt punch for pressing round dimples, dots, and the ends of petals without cutting.
Sharp is not always better here. A blade that cuts cleanly leaves a slick wall the metal slides against; a blunt tool compresses the aragonite and leaves a slightly denser, more defined surface. Try both and watch how the metal reads them.
Depth Control
Work in shallow passes and check depth constantly. A cavity between two and three millimeters deep will fill reliably with a gravity pour; deeper than that and the metal may chill before it reaches the bottom.
For a pendant, aim for a relief that stands one to two millimeters proud of its background. That is deep enough to catch a shadow and shallow enough to fill in one pour.
Press, do not gouge. A gouge tears the fine sheets and leaves a ragged wall that shows up in the casting as a rough, torn edge. A press compacts them into a clean boundary.
Carve Bigger Than You Want
Metal shrinks as it cools — roughly two percent for pewter, closer to three or four for silver, depending on the alloy and the mass of the piece. A cavity carved to exact size will give back a casting slightly smaller than you planned.
In practice, carve your outline a little generous and let the finishing stage bring it back to dimension. This matters most on rings, where a fraction of a millimeter decides whether a piece fits.
Keep a Draft Angle
Walls should lean slightly outward toward the mold face — perhaps five to ten degrees off vertical. This is the draft angle, and it is what allows the casting to slide free instead of keying into the cavity.
Undercut walls, where the cavity is wider at the bottom than at the opening, will lock the metal in place. You will get your casting, but you will get it in pieces, along with a chunk of bone.
Registration: Making the Halves Meet
Two flat faces pressed together will slide. The slightest lateral movement between them during the pour shears the casting in half — a step, a doubled edge, a piece that looks like two drawings printed slightly out of register.
This is the step that ruins most first attempts. It is also the easiest to solve.
Dimples or Pins
The traditional method is a pair of shallow locating dimples. With the faces closed and aligned, press a nail set into the rim of the top bone at two opposite corners, driving it just far enough to mark the lower bone beneath.
Then lift the top bone and press again into those marks, deepening both halves of each dimple. The two cones now nest, and the halves drop into alignment like a lid onto a jar.
Short pins work too. Press two panel pins or cut finishing nails into the lower face so they stand a few millimeters proud, then press the upper face down onto them to mark their seats. The pins do the registering for you.
Place your locators well away from the carved area. A dimple that breaks into the cavity becomes a metal-filled pit, and a pin that wanders into your design becomes a hole in the finished piece.
Sprue and Venting
Metal needs a road in. The sprue is that road: a channel cut from the outside edge of the mold into your cavity, wide enough to carry a column of liquid metal in one continuous flow.
Cutting the Sprue
Choose the highest point of your design, or the thickest part of the form. Metal should arrive somewhere substantial and flow outward into thinner areas, not the reverse.
Cut a channel roughly five millimeters wide at the mold face, tapering to three or four where it meets the cavity. That taper — wider at the top, narrower at the piece — keeps the column fed as the metal cools and shrinks.
Run the channel at a shallow angle, not straight down. A steep drop makes the metal plunge and splash; a gentle ramp lets it slide in and fill from the bottom up.
The Vent
Air already occupies your cavity, and molten metal will not share. Cut a thin vent — a scratch one millimeter wide, no deeper than the point of a pin — from the far edge of the cavity out to the rim of the mold.
The vent should sit opposite the sprue, so the metal pushes air ahead of it and out through the far side. A vent on the same side as the sprue lets air pool in the far corner and leave a rounded void.
Cuttlebone's natural porosity vents some air on its own, which is why the process forgives a missing vent more often than a rubber mold would. But the extra channel costs you ten seconds and saves you a casting.
Melting the Metal
Two metals suit this process, and each wants the same small kit: a crucible, a torch, and a pinch of flux.
Lead-Free Pewter
Lead-free pewter is the beginner's metal: it melts around 230 to 250 degrees Celsius, flows like cream, and will not scale or oxidize the way silver does under a torch. A cheap kitchen torch is enough to melt it.
Buy it as ingot, wire, or scrap marked lead-free, and never use unknown antique pewter, which may contain lead. That is not a precaution to skip. Lead fumes are cumulative and invisible.
Fine Silver
Fine silver melts near 960 degrees Celsius and needs a hotter, more deliberate flame — a plumber's torch or a small melting furnace. It also wants a pinch of flux to keep the surface clean and the melt fluid.
In exchange you get a piece that will not tarnish black in a week and can be stone-set or hallmarked later. For an heirloom-grade pendant, this is the metal to use.
Reading the Melt
Watch the surface. A clean melt goes bright and mirror-like, with a skin that trembles when you move the crucible. That shimmer is the sign that the metal is fully liquid and hot enough to travel.
Dross — a dull, crusty film floating on top — means either oxidation or dirt. Skim it with a scrap of steel or a graphite rod, add your pinch of flux, and let it come back to brightness before you pour.
Do not overheat. Metal pushed past its working temperature absorbs gas, and gas comes back out as bubbles in the casting. A slightly cooler, well-fluxed melt pours better than a blazing one.
Pouring
Preheat the closed mold gently before the pour. Hold it a foot above a low flame for thirty seconds, turning it, until the surface feels warm to the back of your hand.
A cold mold chills the first metal that touches it, freezing a skin before the rest arrives. That skin becomes a seam, a fold, or a place where the fill simply stops.
Hold the two halves firmly closed in one hand, or clamp them between two boards. The pressure must be even and continuous — a mold that opens a hair mid-pour leaks a paper-thin fin across your casting.
Pour in one steady stream, from a height of an inch or two, aimed at the sprue mouth. Keep the stream continuous. A hesitant pour, broken into dribbles, lets each slug of metal skin over before the next arrives.
Fill until metal crowns the sprue and a small dome stands above the mold face. That dome is your reservoir; as the casting shrinks, it feeds metal down the channel.
Quench and Break-Out
Let the mold sit for a few seconds after the pour. Pewter sets almost immediately; silver takes a moment longer. You will see the sprue dome dim and sink slightly as it contracts.
Then drop the whole mold into a bucket of water. The quench is partly practical — it cools the metal fast enough to preserve a fine grain — and partly ceremonial. There is a hiss, a puff of steam, and a smell like a wet stone.
Fishing the mold out, crack it open along the seam. The cuttlebone splits with a soft, dry sound, and there in the hollow is your casting: dull gray, still warm, flawed in ways you did not predict.
That moment is the whole reason people keep doing this. No two are alike, and this one exists because you carved it an hour ago.
Cutting and Finishing the Sprue
Snip or saw the sprue stub free, leaving a millimeter or two proud of the surface. Then file it down flush, working along the length of the stub rather than across it, so you do not drag a gouge into the piece.
Now work through abrasives. Start with 240 grit, then 400, then 800, then 1200 if you want a polish. Change direction between grits so you can see the previous scratches until they are gone.
Burnishing comes last. Rub the surface with a polished steel burnisher or the back of a spoon, pressing hard. This does not remove metal; it compresses the surface layer and pushes it into a soft, deep shine that abrasives alone cannot reach.
For a patina, darken the recesses with a liver of sulfur solution or a commercial antiquing gel, then buff the high points back to bright. The contrast is what makes a shallow relief read at arm's length.
Safety
Metal fumes are the real hazard here, not the flame. Work outdoors or under strong cross-ventilation, with your face out of the plume. Pewter and silver are comparatively tame, but the flux and any impurities are not.
Wear eye protection for every step involving molten metal, and never quench a hot mold over your hand or over a sink you are standing at. Steam expands violently and takes water with it.
Keep water away from the crucible and the pour. A single drop hitting molten metal turns to steam and throws metal outward. Dry your tools, dry your mold, dry your hands.
Use lead-free pewter only. If you cannot confirm an alloy is lead-free, do not melt it indoors, and preferably do not melt it at all.
Three Gift-Ready Directions
Once the process is familiar, the design question becomes the interesting one. Here are three shapes that suit the material.
A Botanical Pendant
Press a real leaf into the soot-blackened face to take an impression, then deepen the veins with a pick. The cuttlebone's fine grain holds the secondary veins, and the casting reads as a leaf rather than a symbol of one.
Leave a small loop of wax or a bent pin at the top of the cavity so the finished piece has a hole to hang from. Drill it afterward if you prefer, but casting the hole saves a step and a broken drill bit.
A Small Initial Tag
Carve a single letter in reverse, at a size no larger than a thumbnail. Block letters with flat walls fill more reliably than script, and the crisp edges of a pressed letter suit the material.
Pewter is the right metal here. A tag is a small, light object, and silver at that size tends to chill before it fills.
Matching Bracelet Charms
Cast one charm, then carve the same motif again in a fresh bone and cast a second. They will differ — the second mold is not the first — and that slight variance is what makes a set feel handmade rather than manufactured.
Three or four charms, each hung from a jump ring, make a bracelet that looks collected rather than bought.
Troubleshooting
Incomplete fill. The metal chilled before it reached the far edge. Preheat the mold longer, widen the sprue, and pour faster and hotter.
Porous, bubbly surface. Gas in the melt or a mold that was too cold. Skim the dross, add flux, and lower your flame so the metal stops absorbing gas.
Misaligned halves. The locators were too shallow, or the mold shifted during the pour. Deepen the dimples and hold the halves with a clamp rather than fingers.
Cracked cuttlebone. Too much pressure during carving or clamping, or a bone that was too thin to begin with. Use thicker bones and press rather than force.
Sprue snapped off inside. Usually a sign the sprue was too narrow at its base. Cut wider next time, and if it happens, drill it out from the back rather than digging at the face.
Conclusion
Your first casting will probably have a rough edge somewhere, a soft corner, a line that did not quite fill. Leave it. Rough edges are part of the tradition — this is a process that has always valued the direct record of the hand over the perfect surface.
The natural next step is to cast the same carved design twice, in two fresh bones, and set the results side by side. The differences will teach you more than any instruction: how your pressure varies, where your depth wanders, which details the material holds and which it loses.
If you find yourself drawn to metal that is shaped rather than poured, Metal Clay Jewelry is a different route to a similar end — a material formed by hand and fired to solid metal, with no mold at all.
But keep a few cuttlebones in the cupboard. There is no faster way to hold an idea in metal, and no method that asks less of you before it gives something back.